Water
Zero Contamination Storage

Built using inert, non-leaching inner surface materials to prevent cross-contamination and maintain ultra-pure water quality.
FRP
Strict Industry Compliance

Engineered to meet stringent global and domestic regulatory standards across pharmaceuticals, biotech, and microelectronics.
Sight Glass
Long-Term Asset Life

High-durability composite and vessel construction reduces long-term replacement cycles and maintenance costs.
Maintenance
Custom Site Engineering

Fully customizable vessel volumes, nozzle configurations, and port arrangements tailored to your facility's exact requirements.

Why Are Vessels for Ultrapure Water Essential?

As a premier manufacturer of Vessels for Ultrapure Water, we supply high-purity storage vessels and pressure containers designed to maintain high water purity levels without leaching contaminants, ensuring full compliance for pharmaceutical, electronic, and food processing applications.
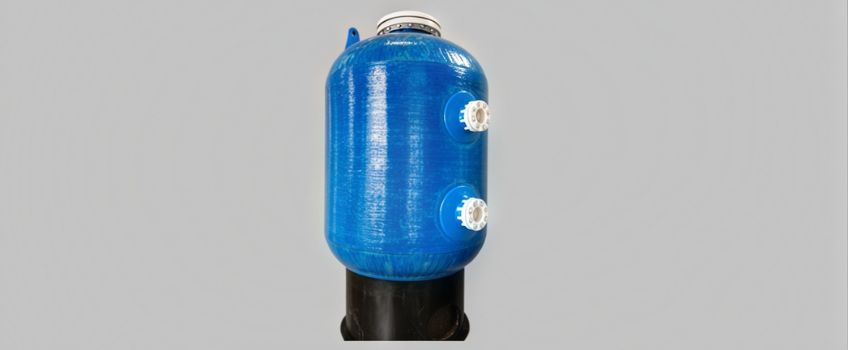
vessel-for-ultrapure-water
  • Critical Quality Preservation: Ultrapure water is an essential commodity across Indian manufacturing, but storing it without quality degradation requires non-reactive, specialized storage media.
  • Total Contamination Prevention: Advanced composite and matrix materials isolate stored liquids from external environmental contaminants and internal ion leaching.
  • Minimized Water Loss: Precision-engineered seal assemblies and high-integrity vessel walls prevent leakage, reducing water loss and keeping operations running smoothly.
  • Indian Manufacturing Expertise: Designed and fabricated by top manufacturers in Mumbai, providing quick delivery, local technical support, and deep familiarity with Indian industrial environments.

Key Features

Inert Non-Leaching Surfaces

Prevents trace organic carbon (TOC) and ionic contamination from leaching into ultrapure fluid streams.

Hygienic Sanitary Fittings

Equipped with smooth-bore sanitary connections and smooth interior finishes to eliminate particle traps and bacterial growth.

High Durability & Strength

Engineered to withstand continuous industrial storage requirements and pressure cycles with minimal physical wear.

Custom Vessel Sizing

Available in a wide range of storage capacities and footprints, from compact skid-mounted tanks to large bulk storage systems.

Full Regulatory Compliance

Assists facilities in meeting strict quality control and safety benchmarks set for pharmaceutical and food-grade operations.

Corrosion & Chemical Protection

High-grade composite materials resist degradation, offering superior resistance compared to standard metallic tanks.

Reduced Infrastructure Footprint

Optimized structural vessel designs maximize storage volume while fitting efficiently into existing cleanroom skids.

Long-Term Advantage

Delivers dependable, long-term performance with minimal maintenance overhead, maximizing return on investment.

Key Advantages of Quality Ultrapure Water Storage

Contamination-Free Preservation

Specialized vessel linings protect against external environmental exposure, particulate ingress, and micro-bacterial growth.

Strict Regulatory Compliance

Helps facilities meet and exceed national and international purity standards required for critical manufacturing processes.

Operational Efficiency

Minimizes fluid loss and prevents costly batch failures caused by water quality degradation during storage.

Long-Service Asset

Exceptional build quality ensures a durable storage solution that requires minimal replacement or structural repair over years of continuous operation.

Industry Applications

  • Pharmaceutical Drug Production: Ensures bulk purified water and water-for-injection (WFI) remain free of particulates and pyrogens, maintaining sterile drug production standards.
  • Semiconductor & Electronics Manufacturing: Protects ultrapure water used in washing high-tech components like semiconductor wafers, preventing trace defects and yield loss.
  • Food Processing & Beverage: Guarantees process water safety, ingredient quality, and hygienic compliance across food and drink manufacturing lines.
  • Medical & Healthcare Facilities: Serves as high-purity storage for laboratory testing, diagnostic equipment, and sterile processing units.

Why Choose Shalin Composites?

  • Trusted Brand in Mumbai: Leading manufacturer of high-performance Vessels for Ultrapure Water, serving diverse industrial clients across India and globally.
  • Uncompromising Purity Standards: Providing long-lasting, customizable composite storage vessels engineered for high-purity applications.
  • Maintain High Operational Standards: Protect your critical water supply, comply with industry regulations, and lower operational costs.
whatsapp