Home -> Products -> FRP Chemical Tank
Expertise in fabricating FRP, PP, PVDF, and PVC tanks tailored to exact fluid temperatures and chemical compositions.
FRP tanks feature a friction-reducing, smooth resin-rich interior layer for superior wear and corrosion resistance.
Fabricated to meet international hygienic standards with thermal insulation, cooling jackets, and CIP integration.
Advanced thermoplastic and composite options offer superior durability and easier installation compared to heavy metal tanks.
As a premier Industrial Tanks Manufacturer in Mumbai, we engineer and fabricate high-performance FRP, Polypropylene, PVDF, and PVC storage tanks designed to securely store chemicals, oil, water, and gases while meeting strict FDA and industrial standards.
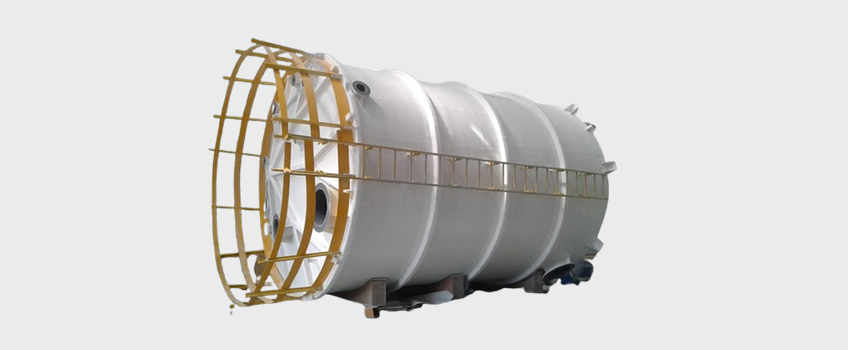
FRP tanks feature a smooth inner wall rich in resin, reducing fluid friction and preventing internal material buildup.
Polypropylene (PP) and PVDF tanks offer exceptional heat retention and stable operation across wide temperature ranges.
PVDF tanks provide high mechanical hardness, low hydrocarbon permeability, and flame retardancy for high-purity lines.
Thermoplastic and composite tanks eliminate rust, weld seam cracking, and corrosion common in metal vessels.
Outdoor bulk storage tanks are built with thermal insulation covers, cooling jackets, and heavy-duty ground anchoring.
Specialized PVC and FRP materials safely contain gasoline, fuel oil, hydrofluorosilicic acid, and corrosive reagents.
Significantly lighter than stainless steel or titanium tanks, reducing infrastructure costs, shipping fees, and setup time.
Built by an experienced frp tank manufacturer capable of customizing vessel geometry, volume, and nozzle layouts.
Known for its exceptional heat resistance, smooth resin-rich inner wear layer, and outstanding chemical resistance. Ideal as a high-durability FRP chemical storage tank for harsh environmental and chemical conditions.
Lightweight, durable, and highly chemical-resistant. Provides a seamless structure with high heat retention and complete immunity to rust and fuel additive corrosion.
Designed for extreme chemical and high-temperature environments, low permeability, high hardness, and flame retardancy. Excellent for high-purity water, semiconductors, and aerospace applications.
Extremely versatile and durable material widely used in the petrochemical industry to contain cracking gasoline, fuel oil, acids, and corrosive liquids.
